If you source pens for a brand, a retail chain, or a distribution network, you already know the frustration. A pre-production sample writes beautifully. Then the first shipment arrives. Half the caps crack in transit, three shades of blue do not match, and customers ask why the ink fades after two weeks.
The gap between a good sample and steady bulk quality usually traces back to one thing: how well you understand the factory’s real process.
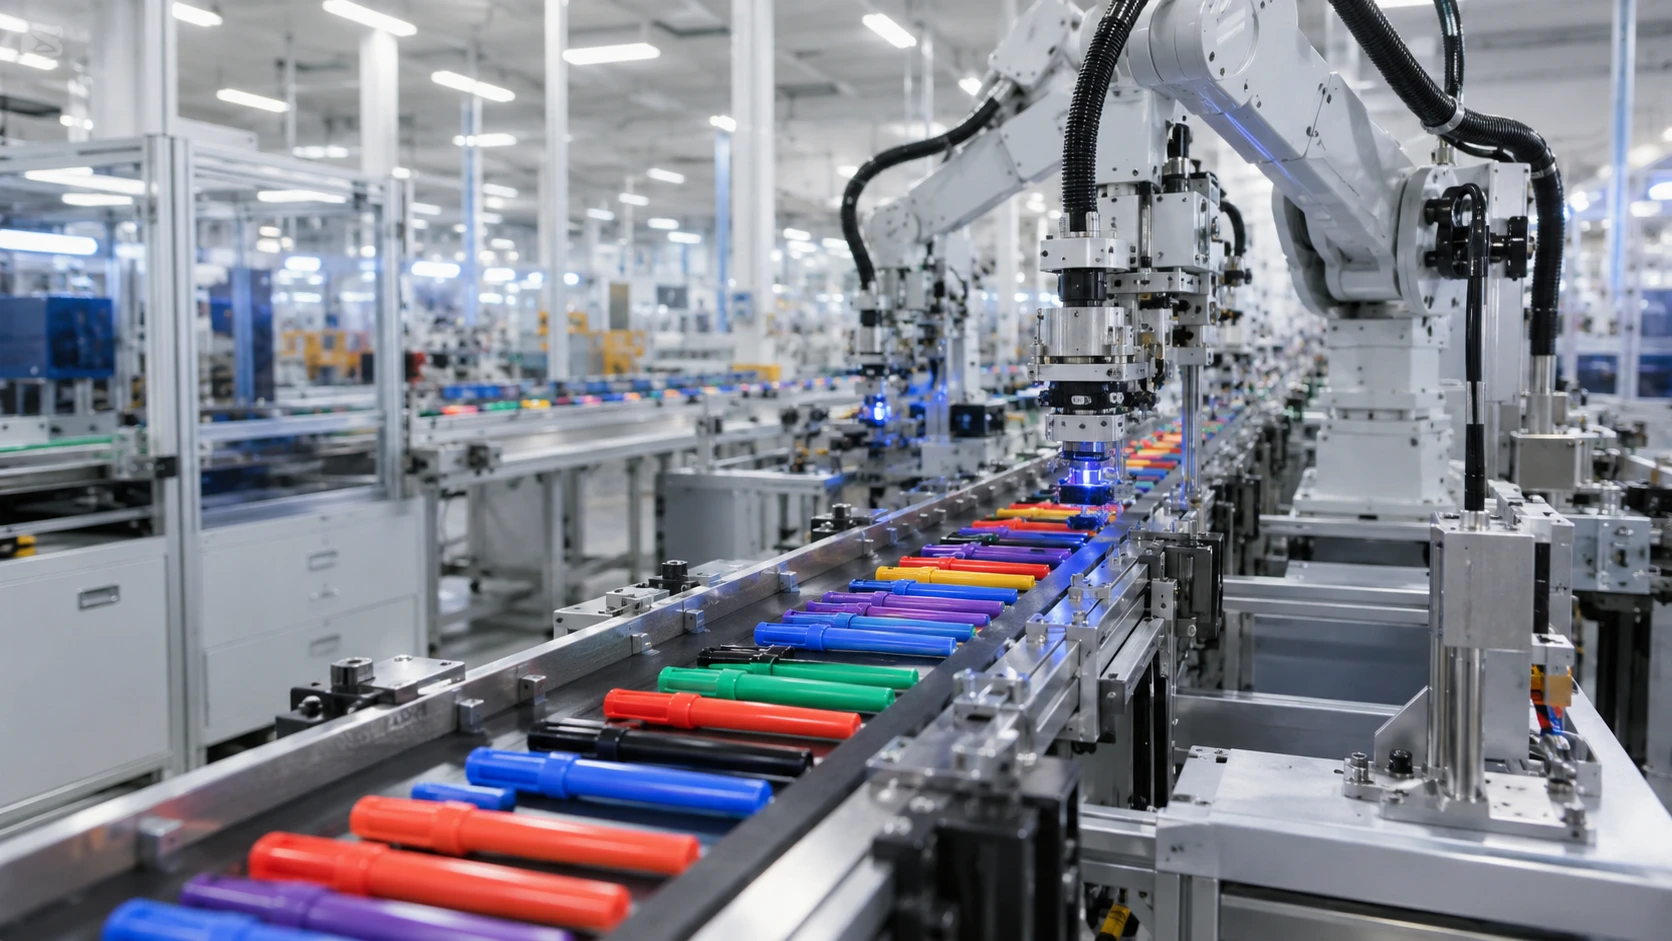
Производство маркеров is not a single step. It is a chain of stages: injection molding, ink mixing, nib assembly, filling, capping, and quality inspection. A weak link anywhere creates problems that grow across an order of 50,000 or 500,000 units.
This guide walks through each stage from a buyer’s view. It shows what happens on the factory floor, what can go wrong, and what to check when you evaluate a supplier. By the end, you will have a practical method to judge whether a manufacturer can deliver consistent quality at scale, not just promise it.
Содержание
Краткий ответ: Что должны знать покупатели B2B о производстве маркеров?
- Marker pen manufacturing has five core stages: barrel molding, ink mixing, nib and wick preparation, automated assembly and filling, and quality inspection
- Injection molding sets dimensional accuracy. Small barrel changes can cause cap-fit failures and leakage at scale
- Ink mixing is the biggest quality variable. Factories that mix ink in-house control color and safety more directly than those buying ready ink
- Assembly combines speed and precision. Automated lines cut human error, but they still need inline checks for fill weight, nib alignment, and cap torque
- Quality control must cover the whole production flow, not just final inspection. Dry-out, skipping, and leakage start at specific stages that floor testing can catch early
For brand owners and buying teams, these five factors help you set sharper sourcing and inspection standards before you commit to bulk production.
Как отказы на этапе производства приводят к типичным дефектам маркеров
If you have handled returns, you know the patterns. Markers dry out in weeks, nibs fray, caps will not stay sealed, and ink comes out pale. Each complaint has a root cause on the production line. Knowing that cause is what separates reactive buying from smart supplier checks.
| Типичная жалоба конечного пользователя | Производственная первопричина | Что следует проверять покупателю на уровне фабрики |
| Маркер быстро высыхает | Недостаточная герметичность колпачка (плохая посадка внутреннего колпачка, недостаточное усилие затяжки колпачка) или рецептура чернил с недостаточным балансом увлажнителя | Тестирование допуска посадки колпачка на автоматизированных станках установки колпачков; тестирование скорости испарения на уровне партии для рецептур чернил |
| Чернила пропускают или пишут бледно | Неравномерная пористость наконечника, захват воздуха во время заправки или вязкость чернил вне спецификации | Спецификация материала наконечника и контроль качества пористости; встроенная проверка веса заправки; записи по вязкости чернил по партиям |
| Несоответствие цвета между партиями | Вариативность источника пигмента или дрейф рецептуры чернил при производстве сторонними поставщиками | Наличие собственной лаборатории чернил; показания спектрофотометра цвета по каждой партии с допуском Delta-E менее 1,5 |
| Трещины корпуса или колпачка | Непостоянная температура литья под давлением или цикл охлаждения, вызывающие внутренние напряжения в пластиковых компонентах | Журналы контроля температуры пресс-форм; протоколы тестов на падение формованных деталей перед сборкой |
| Наконечник истирается или деформируется после ограниченного использования | Некачественный материал наконечника (низкоплотное волокно или неправильное соотношение акрила и полиэстера) | Сертификация материала наконечника от поставщика; тестирование на стойкость к истиранию под контролируемым давлением письма |
| Протечки при транспортировке | Слабая конструкция уплотнения колпачка, недостаточная посадка внутренней заглушки или переполнение чернилами, превышающее допуск на расширение корпуса | Тесты на имитацию высоты/давления; измерение постоянства усилия снятия колпачка на производственных образцах |
Every defect in this table starts at one point on the line. Factories that avoid them are not the ones with the best brochures. They are the ones that monitor and control each stage consistently. Here is what that looks like in practice.
Основные этапы производства маркеров
Marker pen production follows a logical order. For buyers, the point is not to memorize the steps. It is to know where quality is won or lost.
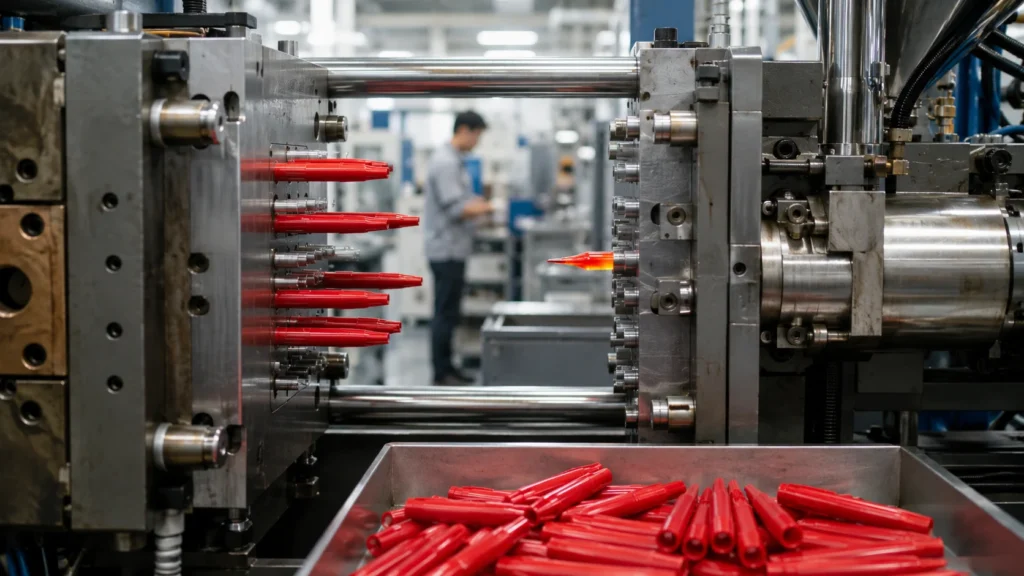
Литье под давлением: где начинается размерная стабильность
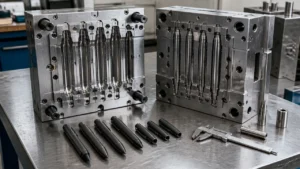
Every plastic part, the barrel, cap, inner cap, and end plug, starts as plastic pellets. A machine melts the pellets and pushes the melt into a steel mold under high pressure. The part cools and hardens, then the cycle repeats, often in under 15 seconds per shot.
Dimensional change can affect cap fit, nib fit, and sealing. Good factories hold the sealing contact points to about ±0.02 mm and the barrel wall to about ±0.05 mm against the drawing. Ask for their dimensional records from the last run, then count the units outside spec before you approve bulk production.
Steady factories differ from unstable ones in mold care. Molds wear down. Blocked cooling lines cause uneven cooling. New material lots change shrinkage. A factory that skips mold logs and maintenance plans will eventually ship barrels that fail the dimensional checks.
At a 10,000+ square meter factory with 8 production workshops, like ZH STATIONERY’s base, molding feeds straight into assembly. Barrel dimensions are spot-checked before parts enter the line. This front-end discipline prevents the cap-fit complaints that arrive months after an order ships.
Состав чернил: основа эффективности маркера
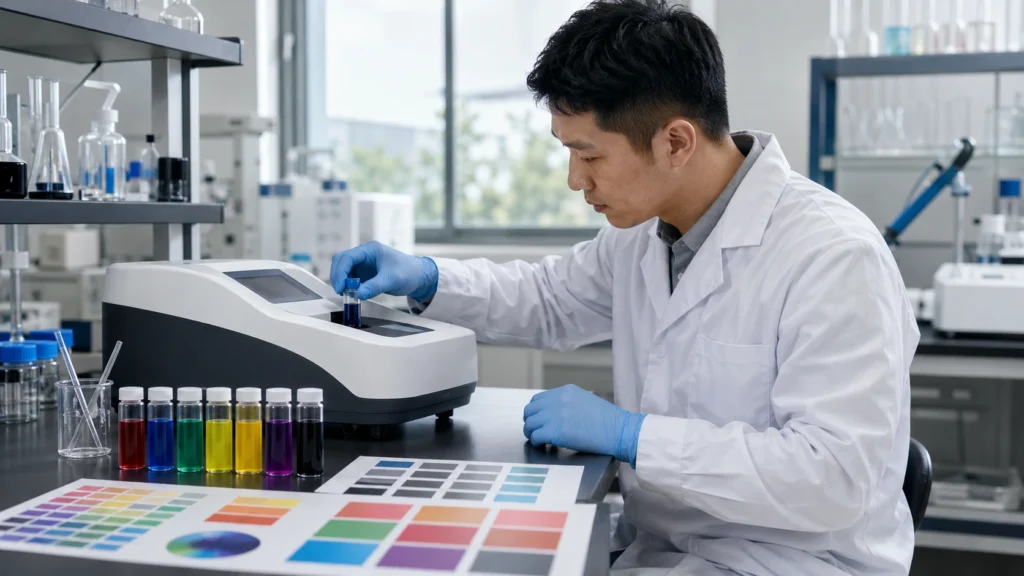
Ink is not just colored liquid. A marker ink mixes five parts: colorant, solvent, resin, humectant, and additives. The colorant gives the color. The solvent carries it. The resin makes it stick. The humectant slows dry-out. The additives control flow and smell. A small mistake in the balance changes color strength, drying time, shelf life, bleed-through, and safety.
This is where in-house ink becomes a sourcing decision, not a footnote. When a factory buys ink from an outside supplier, it inherits that supplier’s variation. Color drift between batches is harder to trace. Safety documents for EN71 and ASTM D-4236 may arrive late or with gaps. Reformulating a custom color becomes a negotiation between several parties instead of an internal fix.
Factories with their own ink lab control the whole flow. Raw pigments come in against a spec. Batch-level color readings confirm the color before ink reaches the filling line. Safety data sheets are made alongside production records, not chased down weeks later. For buyers building программы маркеров под собственной торговой маркой programs with specific colors, in-house ink is a strong sign. It shows color will hold across repeat orders, not just the first one.
Сборка и наполнение: где скорость встречается с точностью
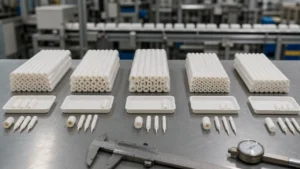
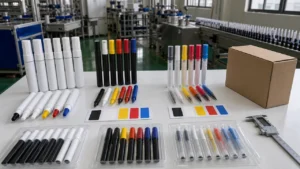
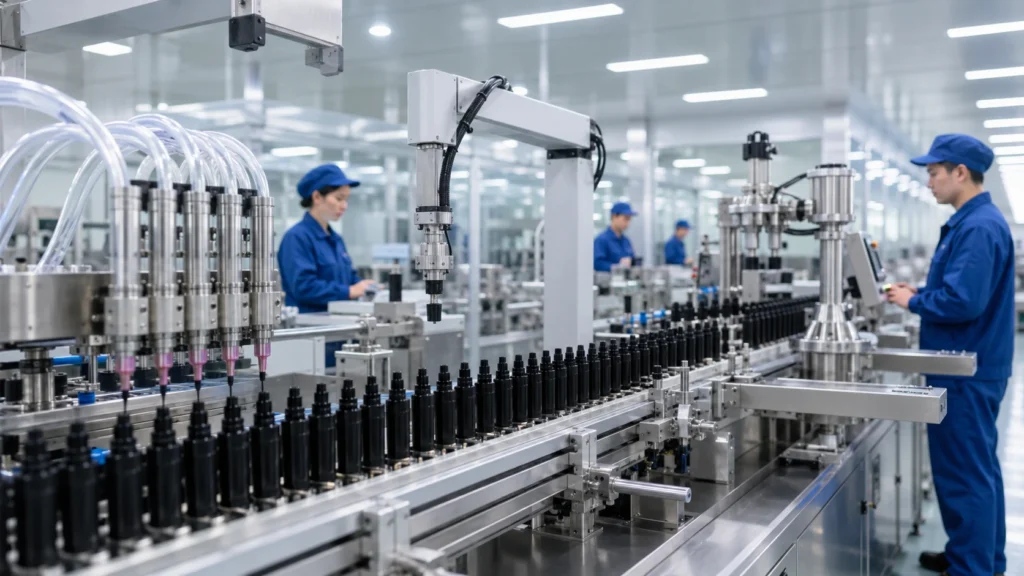
Once the barrels are molded and the ink is batched, the assembly line takes over. In a modern marker pen factory, the line runs an automated sequence. It inserts the nib, places the wick, fills the ink by weight, seals the inner cap, snaps the outer cap, and prints the barrel.
Line speed, fill-weight spread, and defect rate are three separate records. Automated metered filling holds each pen to about ±0.1 g against the target. Ask for the fill-weight spread from the last production run, not just the average, then use the reject count to decide whether filling needs adjustment.
Inline checks matter more than a fast final inspection. Good factories weigh each marker at the filling station and verify cap torque at the capping station. They also pull-test nibs for retention before the packaging belt. When these checks sit inside the line instead of at the end of the shift, defects are caught in real time and fixed at once. When you visit a supplier, ask to see the assembly line running, not just the finished goods area. The line shows whether quality is built in or sorted out later.
Контроль качества: За пределами финальной проверки
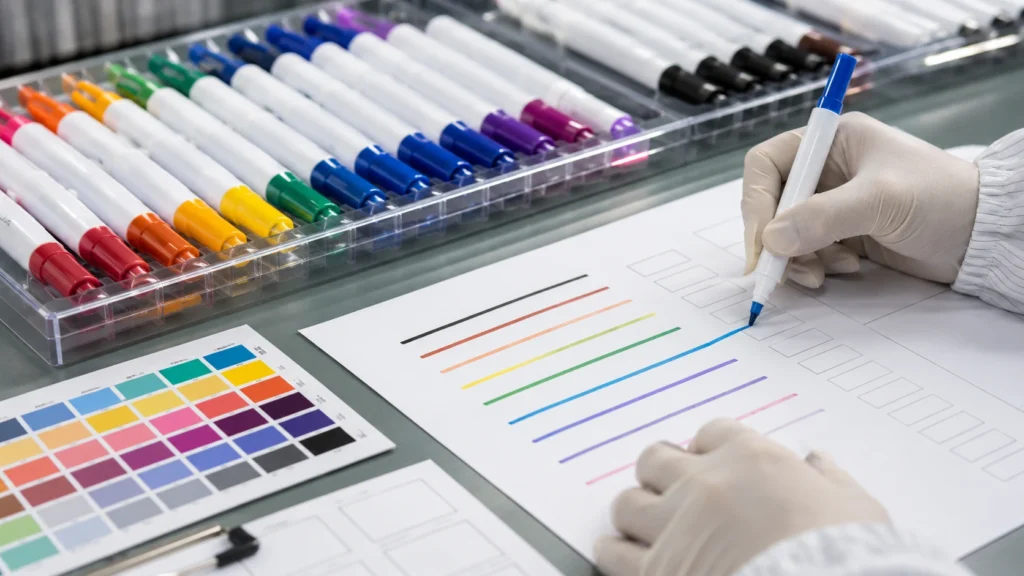
Quality control in marker pen manufacturing should not be one gate at the end. It should be checkpoints across every stage: incoming raw materials, in-process checks on molding, ink, filling, and capping, plus finished goods testing.
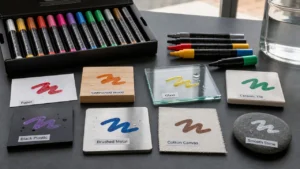
Finished goods testing covers writing, strength, and safety. Writing checks line continuity, color, and dry time; strength checks cap retention, drop resistance, and barrel strength; safety checks heavy metals, phthalates, and volatile compounds. For factories serving the U.S. and Europe, batch-level EN71 and ASTM D-4236 testing should be standard procedure, not an extra the buyer asks for.
One practice separates manufacturing-focused suppliers from trading companies: 100% inline automated inspection before packing. Automated stations check every marker for fill weight, cap torque, and nib retention as it passes. Visual and writing checks run on a strict AQL sample set that clears each lot for shipping. For brands that cannot afford even a 1% complaint rate on the shelf, this matters.
Как качество производства преобразуется в рычаги влияния при B2B-закупках
Understanding the process gives buyers leverage beyond price. When you know which stage causes which defect, you can ask sharp questions on the factory floor during контрольного списка для оценки поставщиков.. You stop relying on a generic promise of quality.
Three areas where this knowledge pays off:
- Постоянство от образца к массовой партии. A pre-production sample is made under easy conditions: slower line, hand-picked parts, extra QC attention. The real test is whether the factory repeats that quality at full line speed across 50,000 units. Ask for inline QC records from a recent run, not just final AQL reports.
- Кастомизация без ущерба. A custom barrel color, a private-label logo, or a new pack format should not shake the process. Factories with mature mold management, in-house ink, and flexible assembly lines can handle customization without new quality risks. A factory with 26+ years of OEM/ODM более 26 лет has learned, across thousands of orders, how to balance custom requests with production stability.
- Документация по соответствию, которая выдерживает проверку. Safety compliance is not a certificate on the wall. It is a chain of records: raw material certificates, batch test reports, third-party lab results, all traceable to specific lots. When a European retailer asks for EN71-3 migration results on one shipment, the factory’s records are either ready or they are not. There is no middle ground.
According to Mordor Intelligence, the global stationery and supplies market reached USD 152.43 billion in 2025. It is forecast to grow at 5.11% per year through 2031. Rising enrollment and corporate buying keep demand steady. For B2B buyers, this growth means more competition at the retail shelf and less tolerance for quality gaps. Understanding the factory process is no longer a nice extra. It is a practical requirement for supplier relationships that last beyond one order.
Сертификаты и индивидуальное производство: что должны проверять покупатели в сегменте B2B
Certificates are easy to list and easy to misunderstand. EN71 is a European toy safety standard with several parts. EN71-3 covers heavy metals that can move out of materials. EN71-9 covers organic chemical compounds. A factory that says it is EN71 certified may hold only Part 3 for a limited product range. The same applies to ASTM D-4236 in the U.S. market: per the Комиссии по безопасности потребительских товаров США, art materials need a toxicology review and a conformance statement, but the standard does not test every possible hazard. Confirm which parts cover your exact product. When you review how a factory manages these records, quality systems built on the ISO 9000 family are a useful baseline.
For private-label marker programs, check manufacturing capability alongside compliance. Key areas to assess:
- The minimum order for custom OEM/ODM programs is 50,000 pens per order, counted by total individual pens produced. For a 12-color pack, that equals roughly 4,200 sets, not 50,000 of each color. Standard stock models can be sampled at smaller trial sizes
- Custom packaging support, including blister cards, display boxes, hang-sell formats, and barcode or UPC integration
- R&D and design support: 3D modeling for custom barrels, physical samples before mold cutting, and Pantone-based color matching
- Ink customization: low-odor formulas, longer cap-off time, or metallic effects instead of a catalog of standard inks
- Sampling workflow: time from design approval to physical sample, and whether the sample comes from the real production line, not hand assembly
A factory that makes over 2,000 new SKUs a year shows ongoing R&D strength, which matters if you plan to refresh your line each season. Combined with in-house ink, 3D design, and automated assembly, you get a partner that supports brand growth, not just one purchase order.
Часто задаваемые вопросы
Какие основные материалы используются при производстве маркерных ручек?
Markers use thermoplastic resin for barrels and caps, usually PP, ABS, or AS. Nibs use polyester or acrylic fiber. Reservoirs use polyester wadding, and ink can be solvent-based or water-based. Material choices affect writing, durability, and safety. For U.S. and European markets, every ink component must meet the relevant standard: ASTM D-4236 in the U.S. and EN71 in Europe, with documented toxicology reviews and batch testing.
Сколько времени занимает изготовление заказа на индивидуальные маркерные ручки?
It depends on the molds. With existing molds and custom branding, production usually takes 25 to 35 days from sample approval to shipment. If you need new barrel or cap molds, add 15 to 25 days for design, machining, and sampling. Add another 7 to 14 days when third-party lab testing is required for EN71 or ASTM D-4236. Rush orders are possible for repeat programs, but first-time custom projects need realistic timing.
Что вызывает высыхание чернил в маркерах, и можно ли это предотвратить?
Dry-out has three main causes in production: cap seal failure, low humectant, and a nib that pulls ink too fast. In a controlled process, cap seal is checked at the capping station, humectant ratios are in the ink record, and wicking is tested during product development. The most common cause in bulk orders is cap-fit variation from worn molds, which is why mold maintenance directly affects marker life.
Какие сертификаты качества должны иметь поставщики маркеров для рынков США и Европы?
For the U.S., ASTM D-4236 conformance is required under the Законом о маркировке опасных художественных материалов. Art materials need a toxicology review and a conformance statement. For Europe, EN71 Parts 3 and 9 apply to products classified as toys, and REACH regulation (EC 1907/2006) limits chemical substances across the EU. Ask for current test reports that name your SKU, not just certificates, and confirm the lab is ISO 17025 accredited.
Каков минимальный объем заказа для изготовления индивидуальных маркерных ручек?
The minimum order for custom OEM/ODM programs is 50,000 pens per order, counted by total individual pens produced. For a 12-color pack, that equals roughly 4,200 sets, not 50,000 of each color. Standard stock models can be sampled at smaller trial sizes.
Как покупатели могут оценить качество маркеров перед размещением оптового заказа?
Ask for a production-line sample, not a hand-assembled sample, because line samples represent bulk quality better. Test writing smoothness, color match across pens, cap fit, and nib strength under pressure. For dry-out, test against the agreed spec: standard alcohol markers hold up for 15-30 minutes uncapped, while low-evaporation water-based designs can reach several hours or more. Review the factory’s internal records: mold logs, ink batch records, fill-weight sheets. If you cannot visit, ask for a video walkthrough of the line and QC stations. What you see on the line tells you more than any verbal promise.
Если вы закупаете маркеры или Металлические маркеры for your brand, связаться с ZH STATIONERY для обсуждения спецификаций, образцов, вариантов упаковки и требований к оптовому производству .
Связанное руководство: Custom Marker Pen Sets: OEM Guide.